Rotary Lobe Pumps
Welcome to our advanced range of rotary lobe pumps, engineered to deliver gentle, low-shear fluid handling that preserves product integrity across low-, medium-, and high-viscosity applications. Built to satisfy the most rigorous sanitary standards and deliver maximum operational reliability, our comprehensive industrial and sanitary portfolio keeps your critical processing lines running at peak performance.
Product Description
Depend on our rotary lobe pumps for virtually pulsation-free handling of all process fluids, regardless of viscosity. Engineered for effortless maintenance and exceptional service life, these pumps offer a broad performance envelope designed to meet diverse operational requirements while maximizing uptime, safeguarding product quality, and boosting plant productivity.
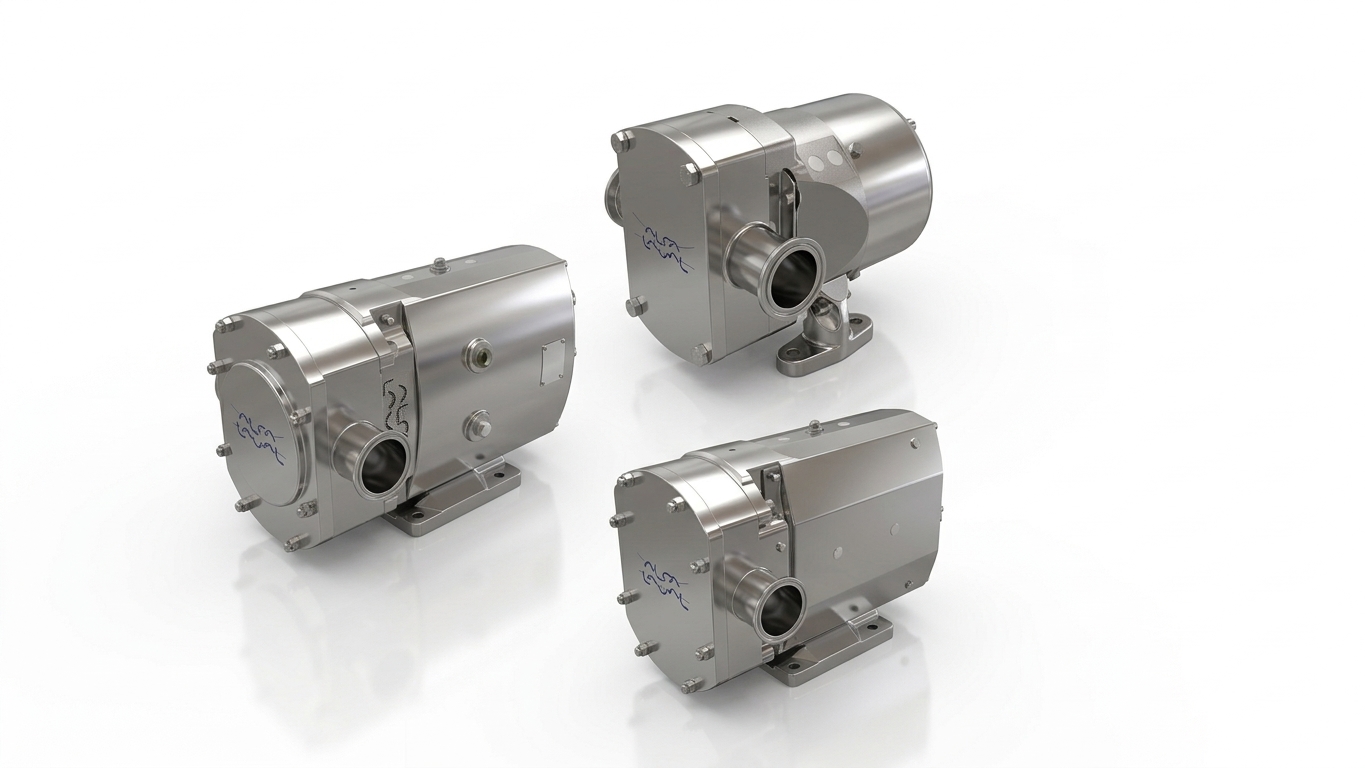
Our versatile pump series caters to distinct operational demands, offering exceptional energy economy, low maintenance costs, and high flexibility:
• OptiLobe Series: Cost-effective, entry-level hygienic pumps optimized for standard transfer duties in food, beverage, and personal care processing.
• SRU Series: Highly adaptable, heavy-duty pumps designed for precise fluid handling across demanding sanitary and industrial applications.
• SX Series: Premium, ultra-hygienic pumps featuring clean-in-place (CIP) design and top-tier compliance for delicate pharmaceutical and sensitive biotechnology processing.
Robust construction, precision tolerances, and gentle product handling ensure ultimate process flexibility and cost-effective operation:
• Reliable, high-performance, low-maintenance pumps engineered for continuous processing with minimal to no unplanned production stops.
• High-quality end-product results achieved through gentle, low-shear pumping action.
• Strict compliance with international hygienic standards for general, food-grade, and pharmaceutical processing requirements.
• Versatile, efficient pumping capabilities tailored for low-, medium-, and high-viscosity fluids.
• Specialized pharmaceutical-grade versions available with comprehensive documentation packages to ensure full supply chain transparency and traceability.
Key Benefits for Industrial & Sanitary Operations
• Gentle Media Handling: Low-shear pumping preserves the delicate structure, color, and overall quality of sensitive fluids and solids-laden media.
• Robust & Compliant Design: Built using premium, durable materials engineered to meet stringent international standards, including EHEDG, 3-A, and FDA requirements.
• Maximum Uptime: Streamlined access for routine maintenance and efficient CIP/SIP cleaning cycles drastically reduce operational downtime.
• Versatile Performance: Efficiently handles fluctuating viscosities, temperatures, and pressures without ever sacrificing flow efficiency.
How Do Rotary Lobe Pumps Work?
Our rotary lobe pumps represent the pinnacle of positive displacement technology, consisting of two intermeshed rotors affixed to a synchronized gear train. The precision-engineered gear train accurately synchronizes the rotors as they rotate in opposite directions.
As the rotors disengage on the inlet side, a expanding cavity forms, creating a partial vacuum that allows atmospheric or external pressure to force fluid smoothly into the pump chamber. As the rotation continues, the fluid is carried around the chamber and discharged into the outlet port as the lobes re-engage. This dependable, continuous displacement mechanism makes our rotary lobe pumps the ideal choice for transferring shear-sensitive fluids and supporting rigorous hygienic processes across multiple industries.