Centrifugal Pumps
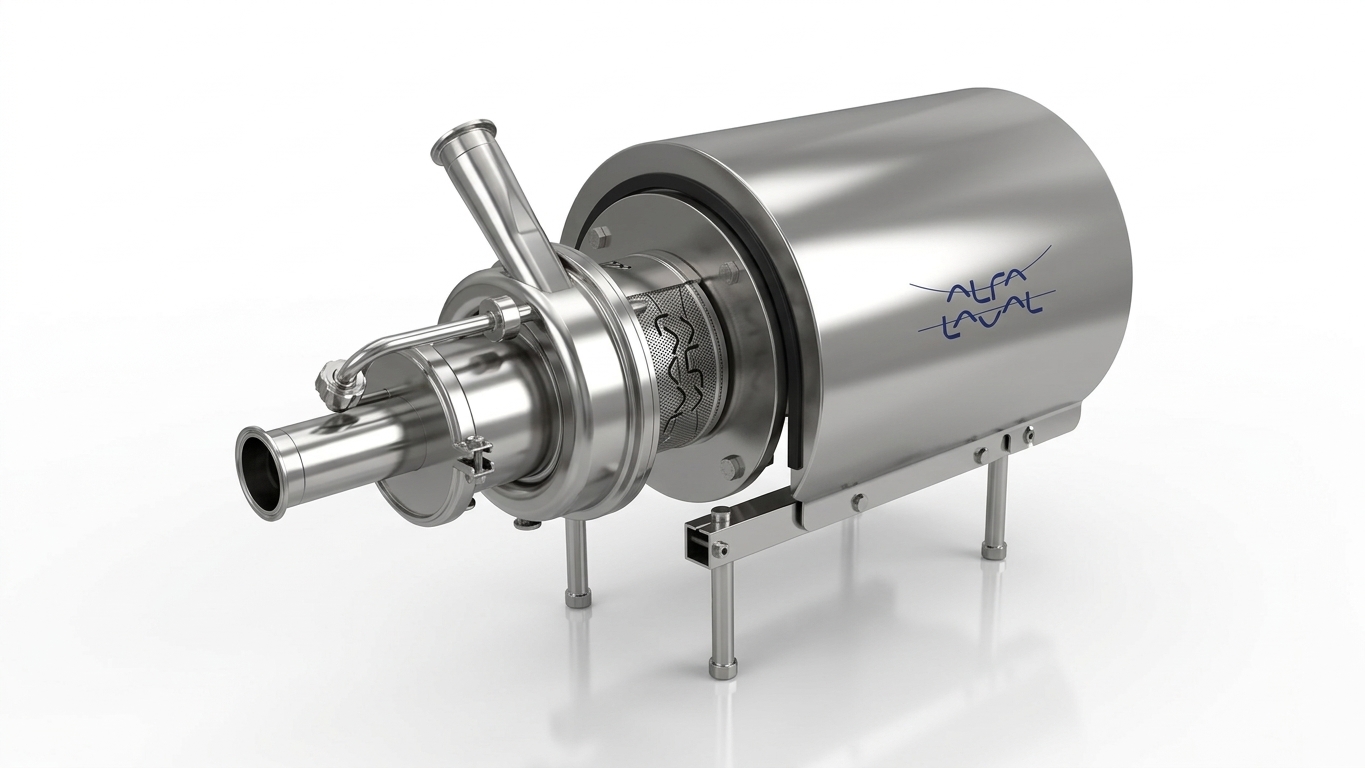
Welcome to Stainless Connection’s premier range of advanced centrifugal pumps, engineered to deliver exceptional efficiency, uncompromising reliability, and an optimized total cost of ownership. Designed specifically for demanding applications across the food, dairy, beverage, and pharmaceutical processing industries, our pumps ensure seamless, hygienic operations while maximizing your facility’s overall productivity and throughput.
Product Description
We offer a diverse and versatile portfolio of centrifugal pump series tailored to meet your exact operational requirements:
• LKH Series (Cost-Effective & High Performance): Expertly engineered for maximum operational efficiency and gentle product handling. This series is ideal for high-pressure systems, evaporation processes, self-priming duties, and high-purity manufacturing.
• SolidC Series (Value & Reliability): Purpose-built for cost-conscious operations where a low initial investment and straightforward, hassle-free maintenance are key priorities.
• MR Series (Self-Priming CIP Return): Specifically designed for Clean-in-Place (CIP) return applications, capable of handling liquids with entrained air or gas smoothly and efficiently without losing prime.
• UltraPure Versions (Pharma & Biotech Grade): Tailored specifically for strict high-purity environments, fully compliant with stringent international pharmaceutical standards and regulations.
Complete Supply Chain Transparency with Q-Doc
To support your strict quality assurance requirements, all our UltraPure models are supplied with a comprehensive documentation package. This ensures complete material traceability, fully transparent supply chain management, and detailed record-keeping of all procedures and spare part modifications. With this documentation, we help you achieve effortless audit compliance and total peace of mind.
Key Features & Operational Benefits
Our centrifugal pump range delivers outstanding performance advantages designed to optimize your plant operations:
• High Efficiency & Low Noise: Delivers exceptional pumping efficiency coupled with low noise levels, making them ideal for demanding tank-emptying and CIP return applications while fostering a safer working environment.
• Uncompromised Hygienic Integrity: Features an advanced hygienic design utilizing FDA-conforming materials and pre-defined compression USP Class VI elastomers, minimizing any risk of process contamination.
• Energy & Resource Savings: Precise hydraulic designs significantly cut energy costs, reduce CO2 emissions, and lower waste chemical volumes, directly boosting your yields and sustainability metrics.
• Maximized Uptime: Robust mechanical construction paired with modular front-loading seals ensures simplified maintenance and maximized operational uptime.
• Reduced Capital Investment: Engineered primarily for CIP duties containing entrained air, these versatile pumps can also handle primary product transfer, reducing the need for additional equipment.
Ensuring a Long Working Life
We build our pumps for exceptional durability and longevity through meticulous engineering and superior craftsmanship:
• Superior Surface Finishes: All product-wetted components feature exceptionally smooth surface finishes down to $RA \le 0.4 \mu m$, significantly reducing the risk of contamination and increasing product yields.
• Optimized Shaft Seal Longevity: The impeller’s precision balance holes generate excellent process fluid circulation around the shaft seal area. This innovative design reduces axial forces and minimizes wear on both the shaft seal and motor bearings.
• Enhanced Cooling and Cleaning: Our hydraulic design ensures high fluid flow around the pump—especially behind the impeller near the shaft seal—facilitating effortless cleaning and superior lubrication and cooling for a substantially extended working life.